Is Your Conveyor System Holding Back Your Operations?
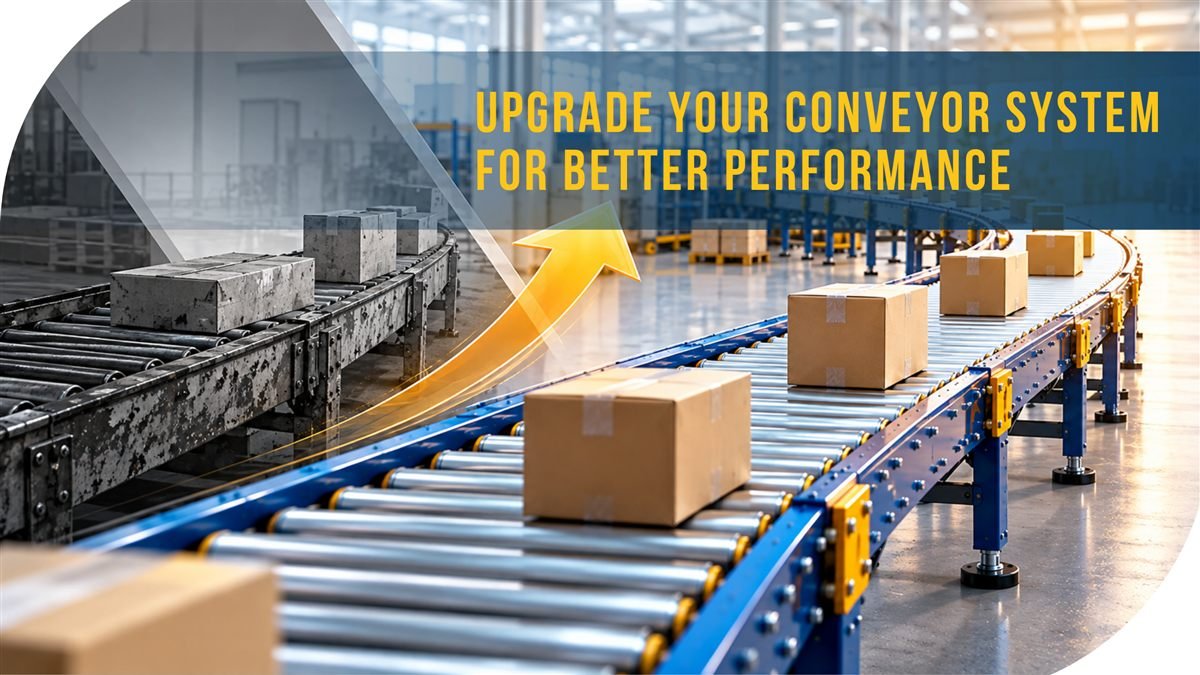
A conveyor system plays a critical role in maintaining smooth, efficient and consistent material movement. However, as production requirements evolve, an ageing or inefficient conveyor system can lead to frequent breakdowns, higher maintenance costs and reduced productivity. Recognising the signs that your industrial conveyor system needs an upgrade can help you improve operational efficiency and prepare your facility for future demands.
Why Conveyor System Upgrades Matter
Conveyor systems are designed to support continuous material movement, but changing production volumes, product specifications and operational requirements can eventually make an existing system less efficient.
Upgrading your conveyor system can help businesses improve:
- Material handling efficiency
- Production throughput
- System reliability
- Workplace safety
- Maintenance efficiency
- Overall operational productivity
Top Signs Your Conveyor System Needs an Upgrade
1. Frequent Breakdowns and Unplanned Downtime
Repeated conveyor breakdowns can disrupt production schedules and increase maintenance costs. If your team is frequently dealing with belt, roller, motor or component failures, your existing conveyor system may no longer be suitable for your operational requirements.
Frequent repairs are often a sign that an upgrade should be considered rather than continuing with recurring maintenance.
2. Rising Maintenance Costs
An ageing conveyor system can require increasingly frequent repairs and replacement of worn-out components.
If maintenance expenses continue to rise, it is worth evaluating whether upgrading to a newer industrial conveyor system could provide better reliability and lower long-term maintenance requirements.
3. Your Production Capacity Has Increased
Business growth often brings higher production volumes. A conveyor system that worked effectively when production was smaller may struggle to keep up with today's requirements.
An upgraded conveyor system can be designed around:
- Higher throughput requirements
- Increased material flow
- New production lines
- Different product dimensions
- Future capacity requirements
4. Material Movement Has Become a Bottleneck
If materials are waiting between production stages or operators are frequently handling products manually, your conveyor system may be creating an operational bottleneck.
A properly designed conveyor layout can help create a smoother flow of materials between different stages of production.
5. Your Conveyor System Requires Excessive Manual Intervention
Modern manufacturing environments increasingly focus on efficient and consistent material movement.
If employees regularly need to manually push, move, reposition or transfer products because the existing conveyor cannot handle the process efficiently, it may be time to evaluate a conveyor system upgrade.
6. Your Existing System Cannot Adapt to Changing Requirements
Manufacturing requirements can change over time. New products, production lines, layouts and material specifications may require a more flexible conveyor solution.
If your existing system cannot easily accommodate these changes, upgrading the conveyor system can provide greater flexibility for future operations.
7. Safety Concerns Are Increasing
Older or poorly maintained conveyor systems can create operational and workplace safety concerns.
Issues such as exposed moving components, damaged parts, improper guarding or inconsistent material movement should be addressed promptly.
A modern conveyor system can incorporate appropriate safety considerations into its design while supporting smoother material handling.
8. Your Energy or Operating Costs Are Increasing
Inefficient equipment can contribute to higher operating costs.
When evaluating a conveyor upgrade, businesses can consider factors such as:
- Drive efficiency
- Conveyor configuration
- Motor requirements
- Material flow
- System utilisation
- Maintenance requirements
A system designed around the actual application can help improve overall operating efficiency.
What to Consider Before Upgrading Your Conveyor System
Before replacing or upgrading your conveyor, evaluate your current operation and future requirements.
Production Requirements
Determine your required throughput, operating hours and expected production growth.
Product Characteristics
Consider product dimensions, weight, shape, surface characteristics and how the product needs to be transported.
Available Floor Space
Your conveyor layout should work within the available production area while maintaining efficient material flow.
Future Scalability
Consider whether the system can accommodate future production expansion, additional conveyor sections or changes in the manufacturing process.
Choosing the Right Conveyor System for Your Application
There is no single conveyor configuration suitable for every manufacturing application. The right solution depends on the product, production process, required speed, load capacity and facility layout.
Depending on the application, businesses may consider solutions such as roller conveyors, belt conveyors, modular belt conveyors and other customised conveyor systems.
The objective should be to create a conveyor solution that supports efficient, reliable and consistent material movement.
Upgrade Your Conveyor System with Excel Conveyors
At Excel Conveyors, we design and manufacture conveyor systems tailored to specific material movement requirements.
From individual conveyor requirements to integrated production-line applications, our solutions are designed with a focus on efficient material flow, reliability and practical industrial requirements.
Looking to Improve Your Existing Conveyor System?
Get in touch with Excel Conveyors.
For business inquiries: sales@econveyors.in
Looking to upgrade your conveyor system? Get in touch with us.