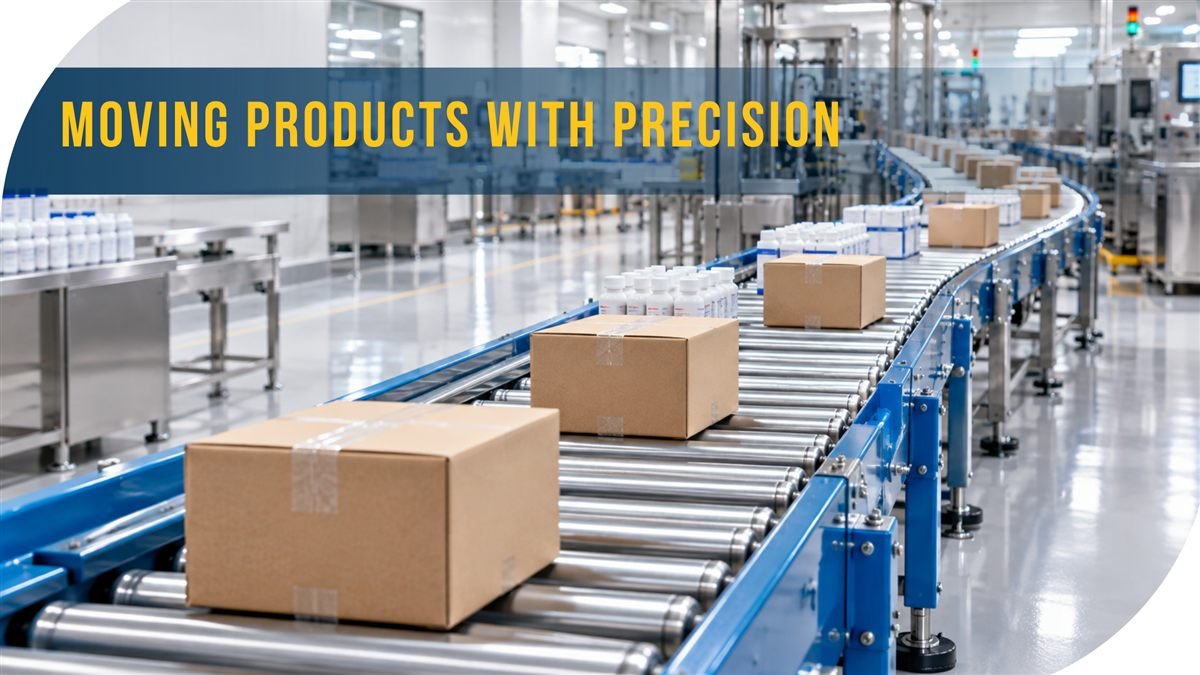
Moving Products with Precision
From pharmaceutical manufacturing to high-speed packaging lines, efficient material movement is essential for maintaining productivity, consistency and operational efficiency. Conveyor systems help automate the movement of products and materials while reducing manual handling and supporting streamlined production workflows.
For industries where hygiene, precision and reliable handling are important, choosing the right conveyor solution can make a significant difference.
The pharmaceutical and packaging industries require reliable conveyor systems capable of handling products efficiently while fitting seamlessly into production and packaging processes.
Depending on the application, conveyors can be used for transporting containers, cartons, bottles, boxes, packs and other products between different stages of production.
Conveyor Applications in the Pharmaceutical Industry
Pharmaceutical manufacturing involves multiple stages where controlled and consistent product movement is required.
Product Transfer and Handling
Conveyors can facilitate the movement of pharmaceutical products and containers between processing, filling, inspection and packaging stages. Automated movement can help reduce unnecessary manual handling and maintain a consistent production flow.
Packaging Line Integration
Pharmaceutical conveyors can be integrated into packaging lines to transport bottles, cartons, containers and other packaged products between different operations.
They can support applications such as:
- Product transfer
- Bottle and container handling
- Inspection processes
- Packing and secondary packaging
- Movement between production stations
The conveyor design can be selected according to product characteristics, line layout and operational requirements.
Conveyor Applications in Packaging
Packaging operations often require continuous and organized product movement. Packaging conveyors can connect different stages of a packaging line and help maintain a smooth workflow.
Transporting Packaged Products
Conveyors can transport cartons, boxes, bottles, pouches and other packaged products from one station to another.
Supporting Automated Production Lines
When integrated with other equipment, conveyor systems can help create a connected material-flow process. This can reduce manual movement and support higher operational efficiency.
Key Benefits of Conveyor Systems
The right conveyor solution can offer several operational benefits:
- Consistent product movement
- Reduced manual handling
- Improved workflow efficiency
- Better utilization of production space
- Easy integration with production lines
- Reliable transportation of products
The appropriate conveyor should always be selected according to the product, load, speed, layout and specific application requirements.
Choosing the Right Conveyor for Your Application
Every pharmaceutical and packaging application has different requirements. Factors such as product dimensions, weight, conveyor speed, available space, operating environment and production workflow should be considered before selecting a conveyor system.
At Excel Conveyors, conveyor solutions are designed to support efficient and reliable product movement across industrial applications.
Whether the requirement involves product transfer, packaging-line movement or connecting different stages of production, selecting the right conveyor design is essential for achieving smooth material flow.
Conclusion
Conveyor systems play an important role in modern pharmaceutical and packaging operations by enabling efficient, consistent and organized product movement.
With the right conveyor configuration, manufacturers can create smoother workflows while reducing unnecessary manual handling and improving overall production efficiency.
Looking for a Conveyor Solution?
Get in touch with Excel Conveyors for your business requirements.
For business inquiries: sales@econveyors.in
Looking for a conveyor solution for your industry? Get in touch with us.